Key Takeaways:
- Overall Equipment Effectiveness (OEE) is a key manufacturing metric that indicates how efficiently a machine or a production line runs during planned production time.
- OEE looks at three factors: Availability, Performance, and Quality.
- Higher Availability means less downtime. Higher Performance means production is closer to the ideal production rate. Higher Quality means the machine or line produces a greater proportion of defect-free products.
- OEE Formula: OEE = Availability x Performance x Quality.
- An OEE of 85% is widely considered a world-class score, yet the average unoptimized plant operates near 60%.
- Genuine OEE improvement requires minimizing equipment losses in availability, speed, and quality, while maintaining sustainable operational standards.
What is OEE in Manufacturing?
Overall Equipment Effectiveness (OEE) is a critical manufacturing metric that evaluates how effectively your production assets run. It measures machine availability, operating speed, and product quality. Expressed as a percentage, OEE’s core objective is to identify production issues and find solutions to improve them.
The higher the OEE score, the better the manufacturing process is performing. Calculated for individual machines and production lines, OEE highlights factors that drag down plant performance. Connecting OEE data to your ERP software helps you determine how production bottlenecks affect costs and profit margins.
Overall Equipment Effectiveness Formula
The OEE formula acts like a fitness tracker for manufacturing. It uncovers how well a manufacturing process is performing compared to its absolute best.
You get to know whether you are facing excessive downtime, running processes that are slower than ideal, or frequently producing parts that do not meet quality standards.
This information is then used to guide the company’s Total Productive Maintenance (TPM) efforts, which are aimed at achieving zero breakdowns, zero defects, and zero accidents.
The standard formula for calculating OEE is as follows:
Where,
- Availability = Run Time / Planned Production Time
- Performance = (Ideal Cycle Time x Total Count) / Run Time
- Quality = Good Count / Total Count
OEE can also be calculated using this formula:
No matter what formula you use, you get the same answer.
Three Components of OEE
OEE is measured using three components, namely, Availability, Performance, and Quality.
Let’s look at each of these components and their significance in OEE calculation.
| Component | What it measures | Example of losses |
|---|---|---|
| Availability | Run time versus planned production time | Changeover time and material shortages |
| Performance | Speed of production or production rate | Slow cycles and minor stops |
| Quality | Good parts versus total parts produced | Rework and scrap |
1. Availability
Availability is the percentage of the planned production time during which the machine actually runs. The time the machine is not running means it has completely halted, which could be due to planned and/or unplanned stops. But both types of stops eat away a portion of the planned production time and are collectively termed as Availability Loss.
Planned stops include die change, tool setup, and mandatory cleaning during production. Unplanned stops, on the other hand, are unexpected issues like die damage and motor failure. Subtract the overall time consumed in both planned and unplanned stop activities from the planned production time, and you get Run Time.
Therefore,
Where,
- Run Time = Planned Production Time – Total Downtime
- Total Downtime = Time consumed in planned and unplanned stop activities
Planned Production Time is the total time during which the machine is ideally expected to run during the shift. Planned production time does not include scheduled breaks like lunch and daily production review meetings.
2. Performance
Performance examines the reason why the production is slower than the ideal production rate. It is either that the machine is running slower than its maximum design speed or there are too many minor stops that reduce the machine’s production output. The slow speed could be attributed to machine wear and tear or poor material being fed into the machine.
On the other hand, a minor stop is a situation where the operator has to briefly stop the machine to clear an obstacle, such as a material blocking the machine flow. A minor stop is too short a time to be counted as Availability Loss. Both slow speed and minor stops are part of Performance Loss.
Where,
- Ideal Cycle Time = Minimum time a machine takes to produce one part
- Total Count = Total number of parts produced during the shift (including good and bad parts)
- Run Time = Planned Production Time – Total Downtime
3. Quality
The third component that affects OEE score is quality. Quality is the percentage of good parts a machine produces against the total parts being manufactured during a shift. It is the Right First Time part. That is, when a machine produces a good part on the very first attempt without requiring any rework.
All other items, such as scrap or defective products requiring minor and major rework, reduce the quality score and contribute to Quality Loss. By measuring this loss, manufacturers can identify the root cause as to why a machine is producing defective products. Quality loss has a direct impact on inventory consumption.
Quality can be expressed as follows:
Where,
- Total Count = All parts produced by the machine, including defective parts
- Good Count = Total Count – Defective Count
How to Calculate Overall Equipment Effectiveness
Calculating OEE requires you to first calculate every component of OEE – Availability, Performance, and Quality. Then multiply all of them to get the final OEE score.
OEE Calculation Example
To understand how overall equipment effectiveness in manufacturing
works in reality, let’s take an example of a precision CNC machine producing high-grade steel gears.
Given information
- Production shift – 9 hours
- Planned breaks – 30 min lunch break, 15 min tea break, and 15 min morning brief
- Planned production time – 8 hours (480 minutes)
- Planned stops – 30 minutes (die change and tool setup)
- Unplanned stops – 63 minutes (coolant line blockage and equipment failure)
- Ideal cycle time – 2 minutes per gear
- Total gears produced – 155
- Defective gears (Rework) – 23
Note – Planned breaks are not included in OEE calculation
Now let’s calculate the three components to find OEE.
1. Calculating Availability
Availability tracks the time the machine was actively running compared to planned production time.
Availability = Run Time / Planned Production Time
- Planned production time = 480 minutes
Run Time = Planned Production Time – Total Downtime
Thus,
- Run Time = 480 minutes − 30 minutes (planned stops) − 63 minutes (unplanned stops)
- Run Time = 387 minutes
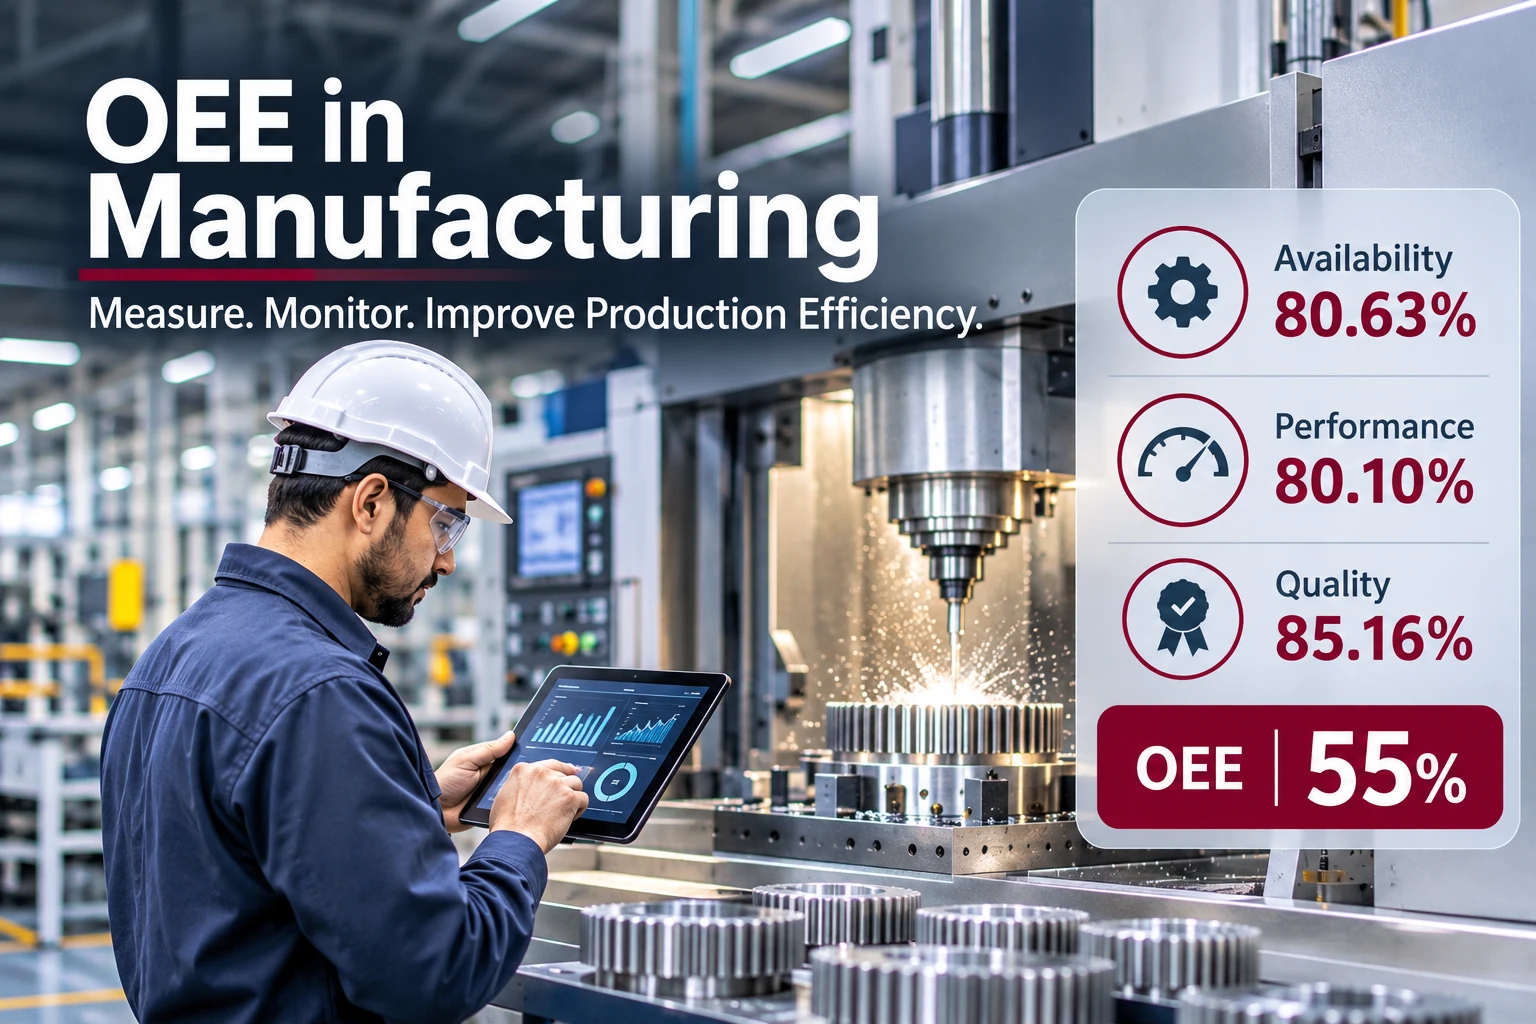
Availability = Run Time / Planned Production Time = 387 / 480 = 80.63%
2. Calculating Performance
Performance tracks how fast the machine produced gears while running compared to its ideal production rate.
Performance = (Ideal Cycle Time x Total Count) / Run Time
- Ideal cycle time = 2 minutes per gear
- Total count = Total gears produced = 155
- Run time = 387 minutes (As calculated above)
Thus,
Performance = (2 x 155) / 387 = 80.10%
3. Calculating Quality
Quality tracks how many gears met quality standards on the first pass without being reworked or scrapped.
Quality = Good Count / Total Count
- Total Count = Total gears produced
- Good Count = Total gears produced – Defective gears
- Good Count = 155 – 23 = 132
Thus,
Quality = 132 / 155 = 85.16%
♥ Calculating OEE
Multiply the three components calculated above to calculate OEE.
OEE = Availability x Performance x Quality
OEE = 0.8063 × 0.8010 × 0.8516 = 55.00%
If we use the other OEE formula, we get the same result.
OEE = (Good Count x Ideal Cycle Time) / Planned Production Time
OEE = (132 x 2) / 480 = 55.00%
Interpretation of OEE
| OEE Metric | Score % | Loss % | Interpretation |
|---|---|---|---|
| Availability | 80.63 | 19.37 | 19.37% of planned production time was lost to setups and machine shutdowns. |
| Performance | 80.10 | 19.9 | During its actual run time, the machine achieved only 80.10% of its ideal throughput. |
| Quality | 85.16 | 14.84 | Out of all the gears the machine produced, 14.84% required rework or were scrap. |
| OEE | 55 | 45 | Only 55% of the planned production time led to defect-free gears at ideal production speed. |
What is a Good OEE Score?
An OEE of 85% is widely accepted as a good OEE score – a world-class benchmark. Of course, you can aim higher as well. Nonetheless, OEE should not be pursued blindly.
Because OEE is highly contextual, what counts as a good score for your factory may not be ideal for another. A number of factors influence this, including product mix, machine setup frequency, preventive maintenance schedules, and tooling limitations.
Ultimately, OEE is a tool for continuous improvement of your internal processes, not for chasing external benchmarks. The most practical approach is to establish your own baseline, measure consistently, and track improvement over time.
If you do compare multiple plants, simply ensure that you use the same methodology.
When a High OEE Score is Actually Misleading
A high OEE score can be misleading in certain situations and it requires your attention. Here’s what can go wrong with the relentless pursuit of OEE.
- Excess production – In a multi-product environment, producing a single product non-stop for longer durations can maximize machine availability by avoiding changeovers. Although OEE increases, it can lead to excess production of a product not needed immediately, thereby increasing inventory holding costs and delaying actual orders.
- More waste – Running machines continuously at their rated capacity might produce more products but can also lead to more scrap and defective pieces due to misfeeding and equipment vibrations. High performance at the expense of poor product quality is not worth pursuing.
- Demotivated employees – Are you putting undue pressure on your staff to work more efficiently? Such pressure increases employee safety risks and puts physical stress on operators. An unhealthy work environment will demotivate employees, hampering your OEE improvement efforts.
Thus, finding the right balance is key to being successful with OEE.
Best Practices for OEE Calculation
- Define your planned production time, excluding periods when production is not scheduled. Apply a consistent policy for breaks and planned maintenance.
- Set the ideal cycle time for each product variant using OEM specifications where available. Otherwise, establish the fastest achievable production rate through a time study.
- If the original equipment has been modified for good reasons, but has permanently reduced output, do take that into consideration for your ideal cycle time calculations.
- For your good count, only count items that pass quality checks the first time, without needing any rework.
- Calculate factory-wide OEE from the combined production data across all lines, accounting for each product’s ideal cycle time. Avoid taking a simple average of individual line OEE percentages.
- Define a consistent threshold for major and minor stops, and log each downtime event only once.
Ways to Improve OEE in Manufacturing
1. Maximize availability
- Apply lean manufacturing principles like Single-Minute Exchange of Die (SMED) to reduce setup times.
- Prepare materials and tooling before production starts.
- Train operators to spot early signs of equipment wear.
- Implement Total Productive Maintenance (TPM) to prevent breakdowns.
2. Optimize performance
- Use sensors to capture minor stops that manual logging may miss.
- Standardize machine settings for each product and investigate recurring speed losses to identify their root causes.
3. Improve quality
- Apply the Pareto principle to prioritize the defects that cause the greatest losses.
- Use poka-yoke (mistake-proofing) wherever possible to prevent incorrect assembly or processing. The technique also helps you detect errors before they lead to further defects.
Also Read: 9 modules of the MES software that efficiently manage production operations
Conclusion
Overall Equipment Effectiveness (OEE) is one of the most sought-after manufacturing metrics used widely across industries. For plants looking to step up efficiency, it is a crucial starting point. By measuring downtime, production speed, and product defects, OEE offers a reality check into what’s lagging and needs to improve.
How Connecting OEE Data to Sage X3 ERP Drives Continuous Improvement
In an efficient factory, sensors, a Manufacturing Execution System (MES) and ERP software work together. Sensors and MES, also known as production software, capture shop floor data used to calculate OEE. Integrating this data with ERP helps manufacturers make better production decisions.
Here are three ways Sage X3 ERP can turn shop floor data into actionable improvements.
1. Reschedule production faster
Sage X3 helps schedule production based on orders, available plant capacity, and machine requirements. When the MES logs a major machine breakdown, Sage X3 can reschedule production orders and reroute jobs to other machines, helping minimize delivery delays.
2. Identify performance losses
Sage X3 keeps a record of your master production routings and standard machine operating times. Its integration with MES allows you to compare actual output against these benchmarks. As a result, bottlenecks and losses caused by minor stops are quickly highlighted.
3. Act on quality issues in real time
When the MES logs a defect, it passes the data to Sage X3. If the defect is due to a machine fault, it can trigger maintenance workflows. If it is because of material issues, X3 automatically places the affected lot on Quality Hold status, blocking the material from being issued to other production lines.
OEE FAQs
1. What Does OEE Mean?
The full form of OEE is Overall Equipment Effectiveness. It measures how well a machine is utilized during its planned production time by looking into machine availability, machine performance, and the quality of products it produces.
2. Is OEE a KPI?
Yes. OEE is one of the most widely used manufacturing KPIs. OEE tracks machine stops, slow running, and defects to generate a consolidated percentage that can be analyzed, compared, and improved.
3. What Does 100% OEE Mean?
100% OEE simply means perfect production. That is to say, the machine works non-stop during planned production time, runs at its ideal speed, and only produces good parts. This is a textbook situation, not possible in reality.
4. What Are The Six Big Losses in OEE?
The Six Big Losses that reduce OEE are categorized under the three core OEE components.
- Availability
a. Equipment failure
b. Setup/adjustments - Performance
c. Idling/minor stops
d. Reduced speed - Quality
e. Process defects
f. Startup losses