Key Takeaways:
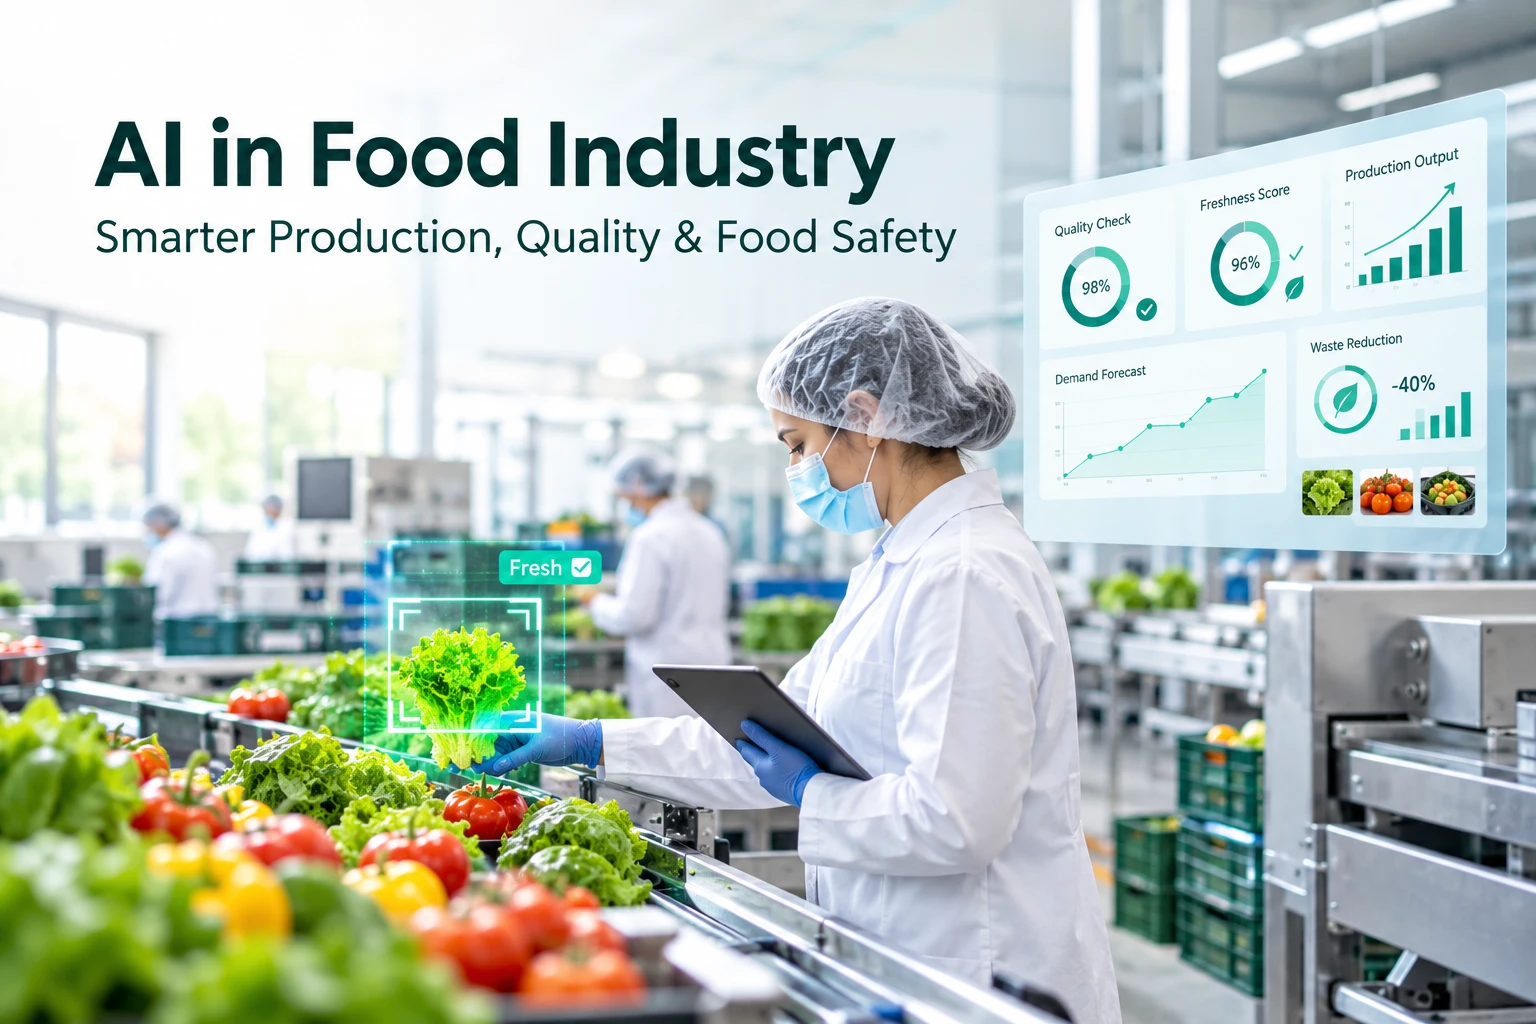
- AI in food industry drives innovation, safety & quality, and operational efficiency through the use of Artificial Intelligence (AI) and Machine Learning (ML).
- AI in food and beverage industry reduces food spoilage risks using automated Computer Vision models and brings end-to-end traceability across batches.
- Artificial Intelligence in food industry supports precise demand forecasting through extensive analysis of historical sales data, seasonal trends, and weather patterns.
- Sage X3 is an AI-powered solution that helps food manufacturers reduce waste, minimise food safety risks, accelerate product innovation, and automate compliance.
What is AI in Food Industry?
AI in food industry is the use of artificial intelligence technology and robotics to set new standards of efficiency across the food supply chain and production, such as driving innovation in new product development, improving food quality and safety and streamlining food sourcing.
Artificial intelligence (AI) is fast gaining popularity in the food business due to its superhuman ability to analyze vast amounts of data using ERP for food industry and smartly predict demand and deliver fresh insights to improve recipe formulations, reduce production costs and minimize food waste.
Real-World Applications of AI in the Food Industry
1. Agricultural Productivity
Farmers are acutely monitoring crop health data, tracking weather patterns, and taking proactive measures to improve agricultural yield. For instance, using real-time data, they can now control temperature and light levels in smart greenhouses. To minimize the impact of pest attacks on crops, farmers can analyze thermal imagery using satellite data.
2. Product Innovation
AI can analyze vast culinary databases using an ERP system to personalize recipes for different taste buds and food cultures. It provides innovative suggestions on healthy ingredient combinations and suggests ways to blend flavors, marking a fundamental shift from traditional research and development mechanisms, and helping save time.
3. Food Manufacturing
Artificial intelligence in food processing and manufacturing assists with food production planning and scheduling of production lines. Through ERP implementation, manufacturers can leverage real-time data analytics to predict equipment failure and avoid production downtime. Besides, food AI can trace contaminants in food production, ensuring quality control and food safety compliance.
4. Food Sorting
Utilizing the power of deep learning, AI in food technology is being used during sorting and grading processes on the food assembly line. For example, food processors can sort fruits based on their size, minimizing manual intervention. Using AI and inventory management software, unwanted raw material can be easily detected, ensuring accuracy and precision in ingredient selection.
5. Food Packaging
It’s remarkable how smart packaging technology is changing the way food is packed. Going beyond the usual flexible packaging, smart packaging helps track temperature and humidity, ensuring quality control of food and extending its shelf life. AI in food technology also aids in packaging material selection and size based on food type.
6. Food Delivery
The application of AI in food industry has enhanced the capabilities of the food delivery process, benefiting food manufacturers, logistics service providers and customers alike. By integrating AI algorithms in the supply chain management software, you can analyze real-time traffic patterns, delivery location and driver and vehicle availability, thus reducing delivery cost and time.
7. Food Retail
The use of AI in food retail assists with forecasting customer demand based on historical data and seasonal variations, a powerful feature found in some of the best ERP software in India. Consequently, retailers can plan procurement and dynamically manage product offerings. This considerably increases the inventory turnover ratio and ensures effective utilization of shelf space.
8. Food Recall Management
Considering the sensitive nature of food, it is not uncommon for food processing companies to recall affected product batches from the market. By tracking real-time data using food AI, food processors can manage product recalls with greater accuracy and cost-effectively. Further, AI-powered food ERP reduces recall instances through enhanced food safety and batch traceability.
9. Sustainability Efforts
AI in food processing is responsible for driving sustainability initiatives of the food business in ways unimaginable before. By focusing on resource efficiency, AI is enabling better water and energy consumption. Through enhanced food production and resource management, organizations are using AI to reduce waste and follow eco-friendly and efficient practices.
What are the Benefits of AI in the Food Industry?
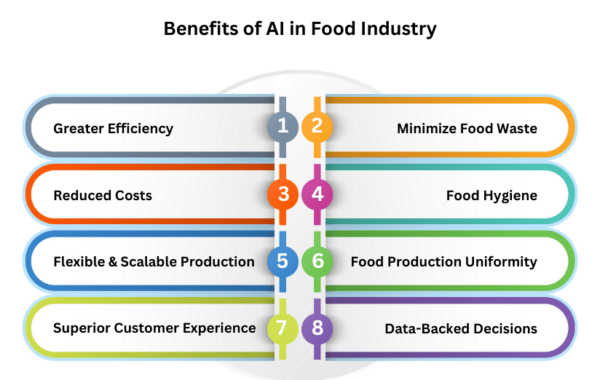
Blending AI and food derives several benefits for the food industry, reshaping how food companies approach challenges. Here are some of the key benefits of AI in the food business.
Greater Efficiency
Be it analyzing market trends to optimize procurement strategies or using AI-powered robots and ERP functions to automate repetitive food production tasks, the implementation of artificial intelligence in food processing industries is enhancing efficiency at every stage of the supply chain.
Minimize Food Waste
Perishable food items such as dairy and meat are always at the risk of getting spoiled and need effective inventory management methods such as FIFO. By integrating AI with IoT sensors, you can track the shelf life of every ingredient and make smarter decisions to reduce food waste and spoilage.
Reduced Costs
AI-enabled demand forecasting model and inventory management system offer actionable insights on what to produce and how much to produce, preventing overproduction. Besides, AI can help food companies optimize resource consumption through production optimization.
Food Hygiene
Maintaining excellent food hygiene is another area where AI in food technology is helping. Advanced data-driven models can detect microbial debris and food residue while ensuring meticulous equipment cleaning and allergen reporting.
Flexible & Scalable Production
AI models embedded within food ERP solutions can track real-time changes in demand from channel partners and suggest changes in food production line. Further, AI makes it simpler and faster to scale production in anticipation of rising demand.
Food Production Uniformity
Food quality, precision and consistency are the defining factors to build trust and brand reputation. With AI in the food supply chain management, it has become possible to enable smarter, quality-focused and more efficient production practices.
Superior Customer Experience
AI models can meet the specific dietary preferences of customers and enable smart product mix management. AI-driven chatbots integrated with ERP software can extract order details and reply to customer queries instantly and accurately, leading to higher customer satisfaction.
Data-Backed Decisions
AI has raised the bar in strategic decision-making with its ability to analyze big data in a matter of seconds. Whether it is analyzing equipment maintenance data powered by predictive analytics or navigating food challenges, AI ensures faster, data-driven responses.
Which AI Technologies Empower Food Businesses?

Looking at the pace of technological innovation, the future of AI in food industry certainly looks promising. Let’s explore how various AI technologies can shape the future of the food business.
1. Generative AI
Analytical AI processes well-structured data to make predictions. Gen AI, on the other hand, has the ability to process large sets of unstructured data to generate new ideas. In agriculture, gen AI can create “what if” scenarios in the ERP software to predict how things might turn out based on weather patterns, soil conditions and pest levels.
2. Computer Vision
Computer vision is the ability of computers to see and interpret things, similar to human vision. In the food industry, computer vision can be easily integrated with your manufacturing ERP software to assess the ripeness of fruits and vegetables on the production line. It can also identify defective products, check labelling data on packaging and ensure precise quantity inside food packets.
3. Artificial Neural Networks
ANNs with interconnected nodes can learn patterns and make decisions, matching intelligence of human brain. These tools hold immense potential in food safety compliance and quality control. By creating AI algorithms of how different microbes grow under varied conditions, ANNs can help predict food safety risk.
4. Robotic Process Automation
Robotic process automation(RPA) simulates human actions to automate repetitive tasks and has wide applications in the food industry. Whichever ERP modules you use, RPA capabilities can be easily built-in, such as AP automation streamlines supplier management by enabling auto-comparison of prices and generating purchase orders.
5. Machine Learning
Machine learning, where computers learn from data and improve their performance, is one of the most significant AI technologies making its presence felt in the food industry. Advanced ERP system uses ML algorithms that can analyze customer feedback and data from IoT sensors on food production machines to identify areas for improvement.
6. Drones and AI
AI-driven drones use aerial data and intelligent insights to monitor crop health by identifying moisture levels, thereby minimizing manual inspections. Drones integrated with warehouse management system can monitor food inventory levels in large warehouses, reducing food waste. AI-guided spraying can optimize fertilizer consumption, spraying only where needed.
7. Blockchain
Blockchain is a breakthrough technology that records transactions in a network of computers to ensure that data can’t be manipulated. Blockchain helps maintain data transparency from food sourcing to production and delivery. During product recalls, food can be easily tracked to its source. Further, it facilitates secure and automated payments between suppliers and food producers.
You May Also Like: How Product Recall plays a vital role in the F&B Industry?
8. Natural Language Processing
Natural language processing is a field of AI that combines artificial intelligence and linguistics. By processing customer feedback data that exists on your ERP system, NLP models can analyze customer sentiment. NLP can also be used for menu analysis for product development, allowing food manufacturers to analyze menus and ingredients in different languages.
9. AR/VR
Augmented Reality (AR) technology projects a digital view of things to understand how they appear before they exist. It is commonly used during prototyping, such as a food distributor looking for new products may ask you to show how the product will look before you begin production.
Similarly, Virtual Reality (VR), often used with VR headsets, can help you to create a simulated environment for customers, allowing them to engage with the product digitally. It can also be used to train staff on food safety protocols in a risk-free digital environment before they begin production.
How AI in Food Manufacturing is Driving Innovation
AI in food manufacturing helps improve demand forecasting accuracy, develop complex food formulas, enhance food traceability, minimise equipment downtime, and optimise production schedules.
1. Forecast Food Demands
Forecasting demand for your food has never been easier. Thanks to AI-powered ERP software, businesses can uncover hidden trends & patterns by analysing large volumes of data such as weather, seasonal changes, and past historical demand for your product.
2. Create & Manage Complex Food Formulas
AI in food industry helps with management and creation of new complex food formulations while predicting taste, texture, nutritional profile, and shelf life. It helps businesses create diverse food products tailored for different customer segments.
3. End-To-End Food Traceability
AI in food ERP automates critical compliance workflows such as batch-level digital record tracking and automated audit preparation, helping you meet the Food Safety Compliance System (FoSCoS) and Food Safety Compliance through Regular Inspection and Sampling (FoSCoRIS) framework.
4. Predictive Maintenance
AI systems directly integrate with the IoT sensors and continuously monitor machine temperature, wear & tear, friction, and error logs. A manufacturer in Gujarat reduced sudden equipment downtimes by 33% using a dedicated AI-powered Maintenance management software.
5. Optimise Production Schedules
AI-powered systems help improve the overall production efficiency by monitoring data retrieved from the IoT-integrated devices and optimising your production schedules accord. By preventing over-production, companies can reduce waste, lower production costs, and achieve a sustainable growth.
How does AI in Food Safety Protect Consumers?
Thanks to AI, businesses can automate food safety, proactively detect food contamination, evaluate freshness of food, predict food safety risks, and continue to adapt to new data.
Food Safety Automation
AI in food safety empowers companies with automated food quality control to ensure consistency in the quality and standardisation across the food safety processes. AI models are trained to detect and flag deviations from quality standards.
Proactively Detect Food Contamination
AI models are trained with a large amount of data to flag appearance defects such as discoloration, deformation, surface damage, spots, and cracks. With automated systems in place, they eliminate the possibility of human errors and oversight in identifying contaminants.
Evaluate Freshness of Vegetables & Fruits
Thanks to AI in food industry and computer vision, businesses can evaluate the freshness of vegetables and fruits, thereby reducing the risk of deviations in quality standards, food spoilage & wastage, and non-compliance.
Predict Food Safety Risks
AI features in Sage X3 actively monitor and predict food safety risks by monitoring historical data pertaining to food contamination, humidity, and temperature. With early detection warnings at your fingertips, you can prevent food risks from adverse weather conditions, humidity and storage conditions.
Continue to Learn & Adapt to New Data
AI in food and beverage industry algorithms are trained with massive datasets. They continue to learn and adapt to new data, thereby improving the overall accuracy of the quality standards and improving overall customer satisfaction.
How can companies implement Artificial Intelligence in Food Manufacturing?
Here’s the step by step guide to deploy an AI-powered food ERP software in your company:
Evaluate Your Business Workflows
First things first, evaluate your organisation-wide processes and thoroughly examine the workflows that can be improved with the AI in ERP. For example, formula management, demand forecasting, production scheduling, order tracking, and customer service.
Data Collection
The next step is to consolidate data from different departments and sources with a centralised ERP system. This will help you effectively evaluate the performance of business processes using various KPIs and make strategic decisions.
Technological Compatibility
Many businesses still rely on obsolete disconnected tools. While these tools are cost-efficient, they serve only specific purpose and do not actively support data synchronisation.
Technological Upgradation
If you’re still relying on spreadsheets and disconnected legacy tools, it’s time to upgrade to an enterprise-wide solution. An AI-powered Cloud ERP can be a handy option; as it doesn’t come with huge upfront costs and provides you the flexibility & customisability needed to achieve your goals.
Employee Training
Mere technological upgradation may not yield results without comprehensive employee training. Train your employees to efficiently use the Artificial Intelligence in food industry and reduce the potential for human errors & inefficiencies.
Ongoing Monitoring & Employee Feedback
Deploy the AI in food safety system organisation-wide in a phased manner to avoid potential disruptions in the business operations. Once the system is deployed, actively monitor its performance, gather employee feedback, and fix any issues.
Lead the Food Industry with AI-powered Capabilities
AI algorithms have become an integral part of the food industry, revolutionizing the traditional approach to food supply chain management. As food processing companies scale their operations using ERP for food industry, artificial intelligence is set to take center stage, helping you gain a competitive edge with precise data-backed decisions.
With intelligent and efficient ERP software like Sage X3, you can integrate all of the AI-driven technologies to shape the future of your food operations. Be it procurement, production, R&D or inventory, Sage X3 has all it takes to set new standards of business excellence, enhance customer experience and reduce production costs.
Frequently Asked Questions (FAQs) on Ai in Food Industry
1. How does AI help detect food spoilage & contamination?
Here’s how AI in food and beverage industry help detect food spoilage and contamination:
- Prevents Food Spoilage: Analyses temperature, humidity and other data received from sensors to prevent food spoilage & waste.
- Identifies Visual Defects: Detects food discoloration, mould and contamination to prevent health risks and safety deviations.
- Predicts Food Spoilage: Analyses historical data about food spoilage, environment and storage conditions to predict potential spoilage.
- Forecasts Product Shelf-Life: Helps food manufacturers predict the shelf-life of their food products.
- Flags Quality Deviations: Automated quality control systems in place to flag deviations and potential safety issues.
2. Does AI in food manufacturing help reduce food wastage & spoilage?
Absolutely! Artificial Intelligence in food industry helps businesses accurately forecast demand for their products, avoiding the risk of over-stocking and food wastage. With early alerts about food contamination & spoilage, it helps businesses protect entire batches from being lost.
3. What are the traceability benefits of AI in food industry?
AI-powered systems help food manufacturers achieve end-to-end traceability while reducing potential delays in the entire procedure. By maintaining digital traceability records, they can seamlessly retrieve the information during audits and food safety investigations, and ensure better compliance.
4. How does AI promote food innovation?
Here’s how AI promotes food innovation:
- Ingredient Optimisation: AI-powered systems help creation of complex product formulas that meet diverse customer requirements.
- Personalised Nutrition: AI takes customer dietary preferences, lifestyle factors and health data into consideration for recommending tailored food products.
- Speeds Up R&D: AI cuts down the time in manual paperwork and reduces inefficiencies at different levels.
- Predictive Risk Monitoring: AI builds a proactive framework to reduce the risk of food spoilage & wastage.
5. What are the common Artificial Intelligence in food industry examples?
Here are the most common Artificial Intelligence in food industry examples:
- Food Quality Automation: Detect food quality issues, discolouration, and damage.
- Food Spoilage Alerts: Automatically flag early signs of food spoilage.
- Contamination Alerts: AI analyses sensor readings to find food contamination risks.
- Predictive Maintenance: Detect equipment failure early and avoid downtimes.
- Production Optimisation: Automated production planning, inventory optimisation, and demand forecasting.